Explore our top-tier manufacturing output engineered for medical facilities, hospital power backup, emergency field operations, and industrial medical applications.
The global healthcare procurement landscape has undergone a structural paradigm shift. As hospital networks, emergency response units, government healthcare authorities, and medical device distributors re-evaluate their supply chain vulnerabilities, China’s position as the primary hub for medical supply manufacturing and supporting energy infrastructure has evolved from simple low-cost volume production to highly sophisticated, technology-driven OEM/ODM manufacturing ecosystems.
Modern medical manufacturing requires an unprecedented synthesis of metallurgical precision, cleanroom bioprocessing, electronic reliability, and uninterrupted electrical power architecture. Sourcing from accredited Chinese manufacturers allows global buyers to leverage integrated industrial clusters where raw materials, precision injection molding, micro-electronics, automated assembly, and stringent QA/QC protocols coexist within tightly linked industrial corridors.
Key Insight for Procurement Officers: Evaluating a wholesale manufacturer in China extends beyond unit price. World-class buyers analyze Total Cost of Ownership (TCO), regulatory compliance track records (FDA 510(k), CE MDR, ISO 13485), sub-component supply continuity, and critical backup power resilience (IEC 60601-1 electrical safety standards).
Whether procuring disposable Class I medical consumables, Class II diagnostic machinery, mobile emergency transport solutions, or hospital-grade uninterruptible energy storage (ESS) systems, global sourcing managers must systematically evaluate vendor capabilities against international regulatory benchmarks and audited factory standards.
Rigorous Quality Management Systems certified for medical device production, full batch traceability, cleanroom validation, and CE MDR / FDA compliance support.
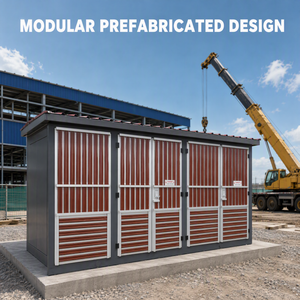
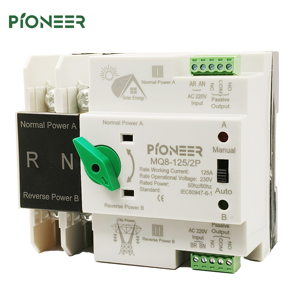
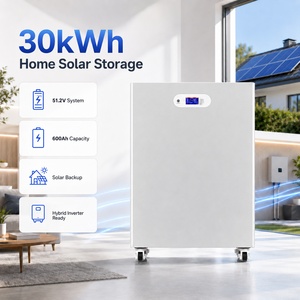
Hospital-grade power redundancy systems including 10kV-35kV prefabricated substations, Automatic Transfer Switches (ATS), and LiFePO4 battery energy storage (ESS).
Full-spectrum contract manufacturing services from CAD enclosure prototyping to custom PCB layout, internal BMS programming, and specialized packaging designs.
Our manufacturing matrix operates at the intersection of heavy electrical engineering and ultra-clean medical supply production. To support critical healthcare facilities and global B2B distribution partners, our production facilities incorporate advanced automation, multi-tier inspection protocols, and robust quality control architectures.
Products designated for patient care, diagnostic interfacing, and clinical environments are manufactured in Class 100,000 (ISO Class 8) and Class 10,000 (ISO Class 7) positive-pressure cleanrooms. Automated optical inspection (AOI) units, robotic ultrasonic welding, and bio-burden monitoring ensure every unit batch conforms to bio-compatibility and sterility standards.
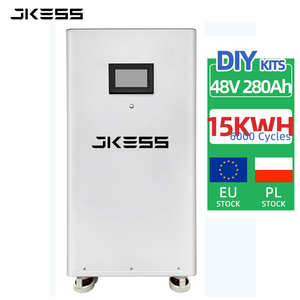
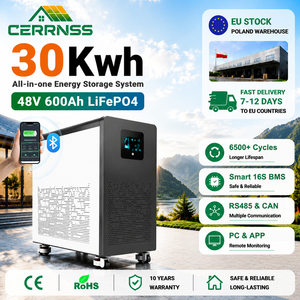
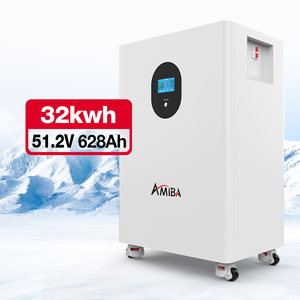
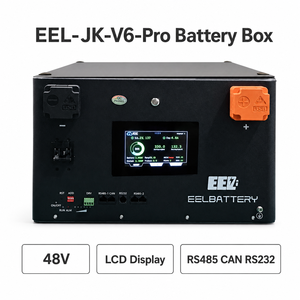
Modern hospitals and field medical stations cannot tolerate millisecond power interruptions. Our manufacturing ecosystem integrates high-capacity 51.2V LiFePO4 energy storage racks (280Ah/300Ah configurations), automatic dual-power transfer switches (ATS 100A), and 10kV-35kV outdoor compact substations. These systems ensure that critical care ventilators, surgical suites, and diagnostic imaging equipment maintain continuous operation during grid instability or emergency disaster recovery.
Every raw material batch—from medical-grade polymers and stainless steel alloys to LFP battery cells—undergoes incoming material inspection (IQC). We enforce full material traceability, providing incoming material certifications (MTC), RoHS/REACH compliance documentation, and complete testing logs (OQC) prior to container loading.
As healthcare systems transition toward digitized, decentralized, and environmentally sustainable operational models, purchasing managers must align their 5-year procurement strategies with emerging industry trends:
Medical energy backup systems and mobile medical equipment are increasingly equipped with smart IoT telemetry. Modern LiFePO4 energy storage systems feature remote Bluetooth/RS485/CANbus BMS interfaces that allow hospital engineers to monitor cell voltages, state of charge (SoC), thermal parameters, and cycle counts in real time, switching from reactive maintenance to predictive health diagnostics.
Global humanitarian relief, military field medical units, and rural healthcare clinics are rapidly adopting off-grid microgrids. Combining transportable, dual-suspension mobile transport units with modular 48V stackable energy storage boxes and quick-deploy compact substations enables rapid deployment of fully functional field clinics within hours of disaster onset.
In response to international carbon mandates and customs logistics complexity, top-tier Chinese manufacturers are establishing regional warehouse hubs (e.g., EU-Stock duty-free nodes). This model allows B2B buyers to access pre-cleared, tax-paid inventory locally, dramatically reducing lead times from 45 days of ocean transit to 72-hour regional dispatch.
In the competitive OEM market, manufacturers who invest heavily in R&D and advanced materials offer significant information gain and operational advantages to global distributors. Key product developments include:
Our primary production facilities operate under ISO 13485 (Medical Devices Quality Management) and ISO 9001:2015 standards. Specific medical product lines comply with CE MDR (EU 2017/745), US FDA 510(k) guidelines, and RoHS/REACH environmental directives. Electrical equipment (such as ATS, Lifepo4 storage, and substations) carries CE, IEC 62619, UN38.3, and MSDS clearance documentation.
Yes. We offer comprehensive OEM/ODM services including custom chassis industrial design, firmware customization (BMS protocol matching with major inverter brands such as Victron, Growatt, Deye, Sofar), specialized packaging, custom color powder coating, and branded labeling to meet distributor specification sheets.
For standard catalog items or EU/US regional warehouse stock, dispatch occurs within 3 to 7 business days. For bulk OEM factory runs, sample production requires 10-15 business days, while full container load (FCL) orders typically ship within 25-35 calendar days following engineering drawing approval.
All lithium iron phosphate (LiFePO4) battery packs undergo 100% cell matching (capacity, internal resistance, voltage testing), high-voltage isolation tests, and thermal stress testing. Ocean freight shipping is accompanied by official UN38.3 transport certification, Dangerous Goods (DG) declarations, and certified drop-tested UN boxes.
We provide a standard 5-year warranty on metal-enclosed power storage units and electrical substations, expandable to 10 years for premium LFP storage systems. Warranty claims are handled via direct engineering support, providing replacement modules, active BMS boards, or full unit replacement with fast-track global courier delivery.
Request direct factory pricing, technical whitepapers, engineering datasheets, or custom OEM quotes for your medical and power infrastructure projects.
Contact Us